Understanding Shaftless Screw Conveyor Equipment: An Innovative Solution for Efficient Material Handling
Mar 14,2026
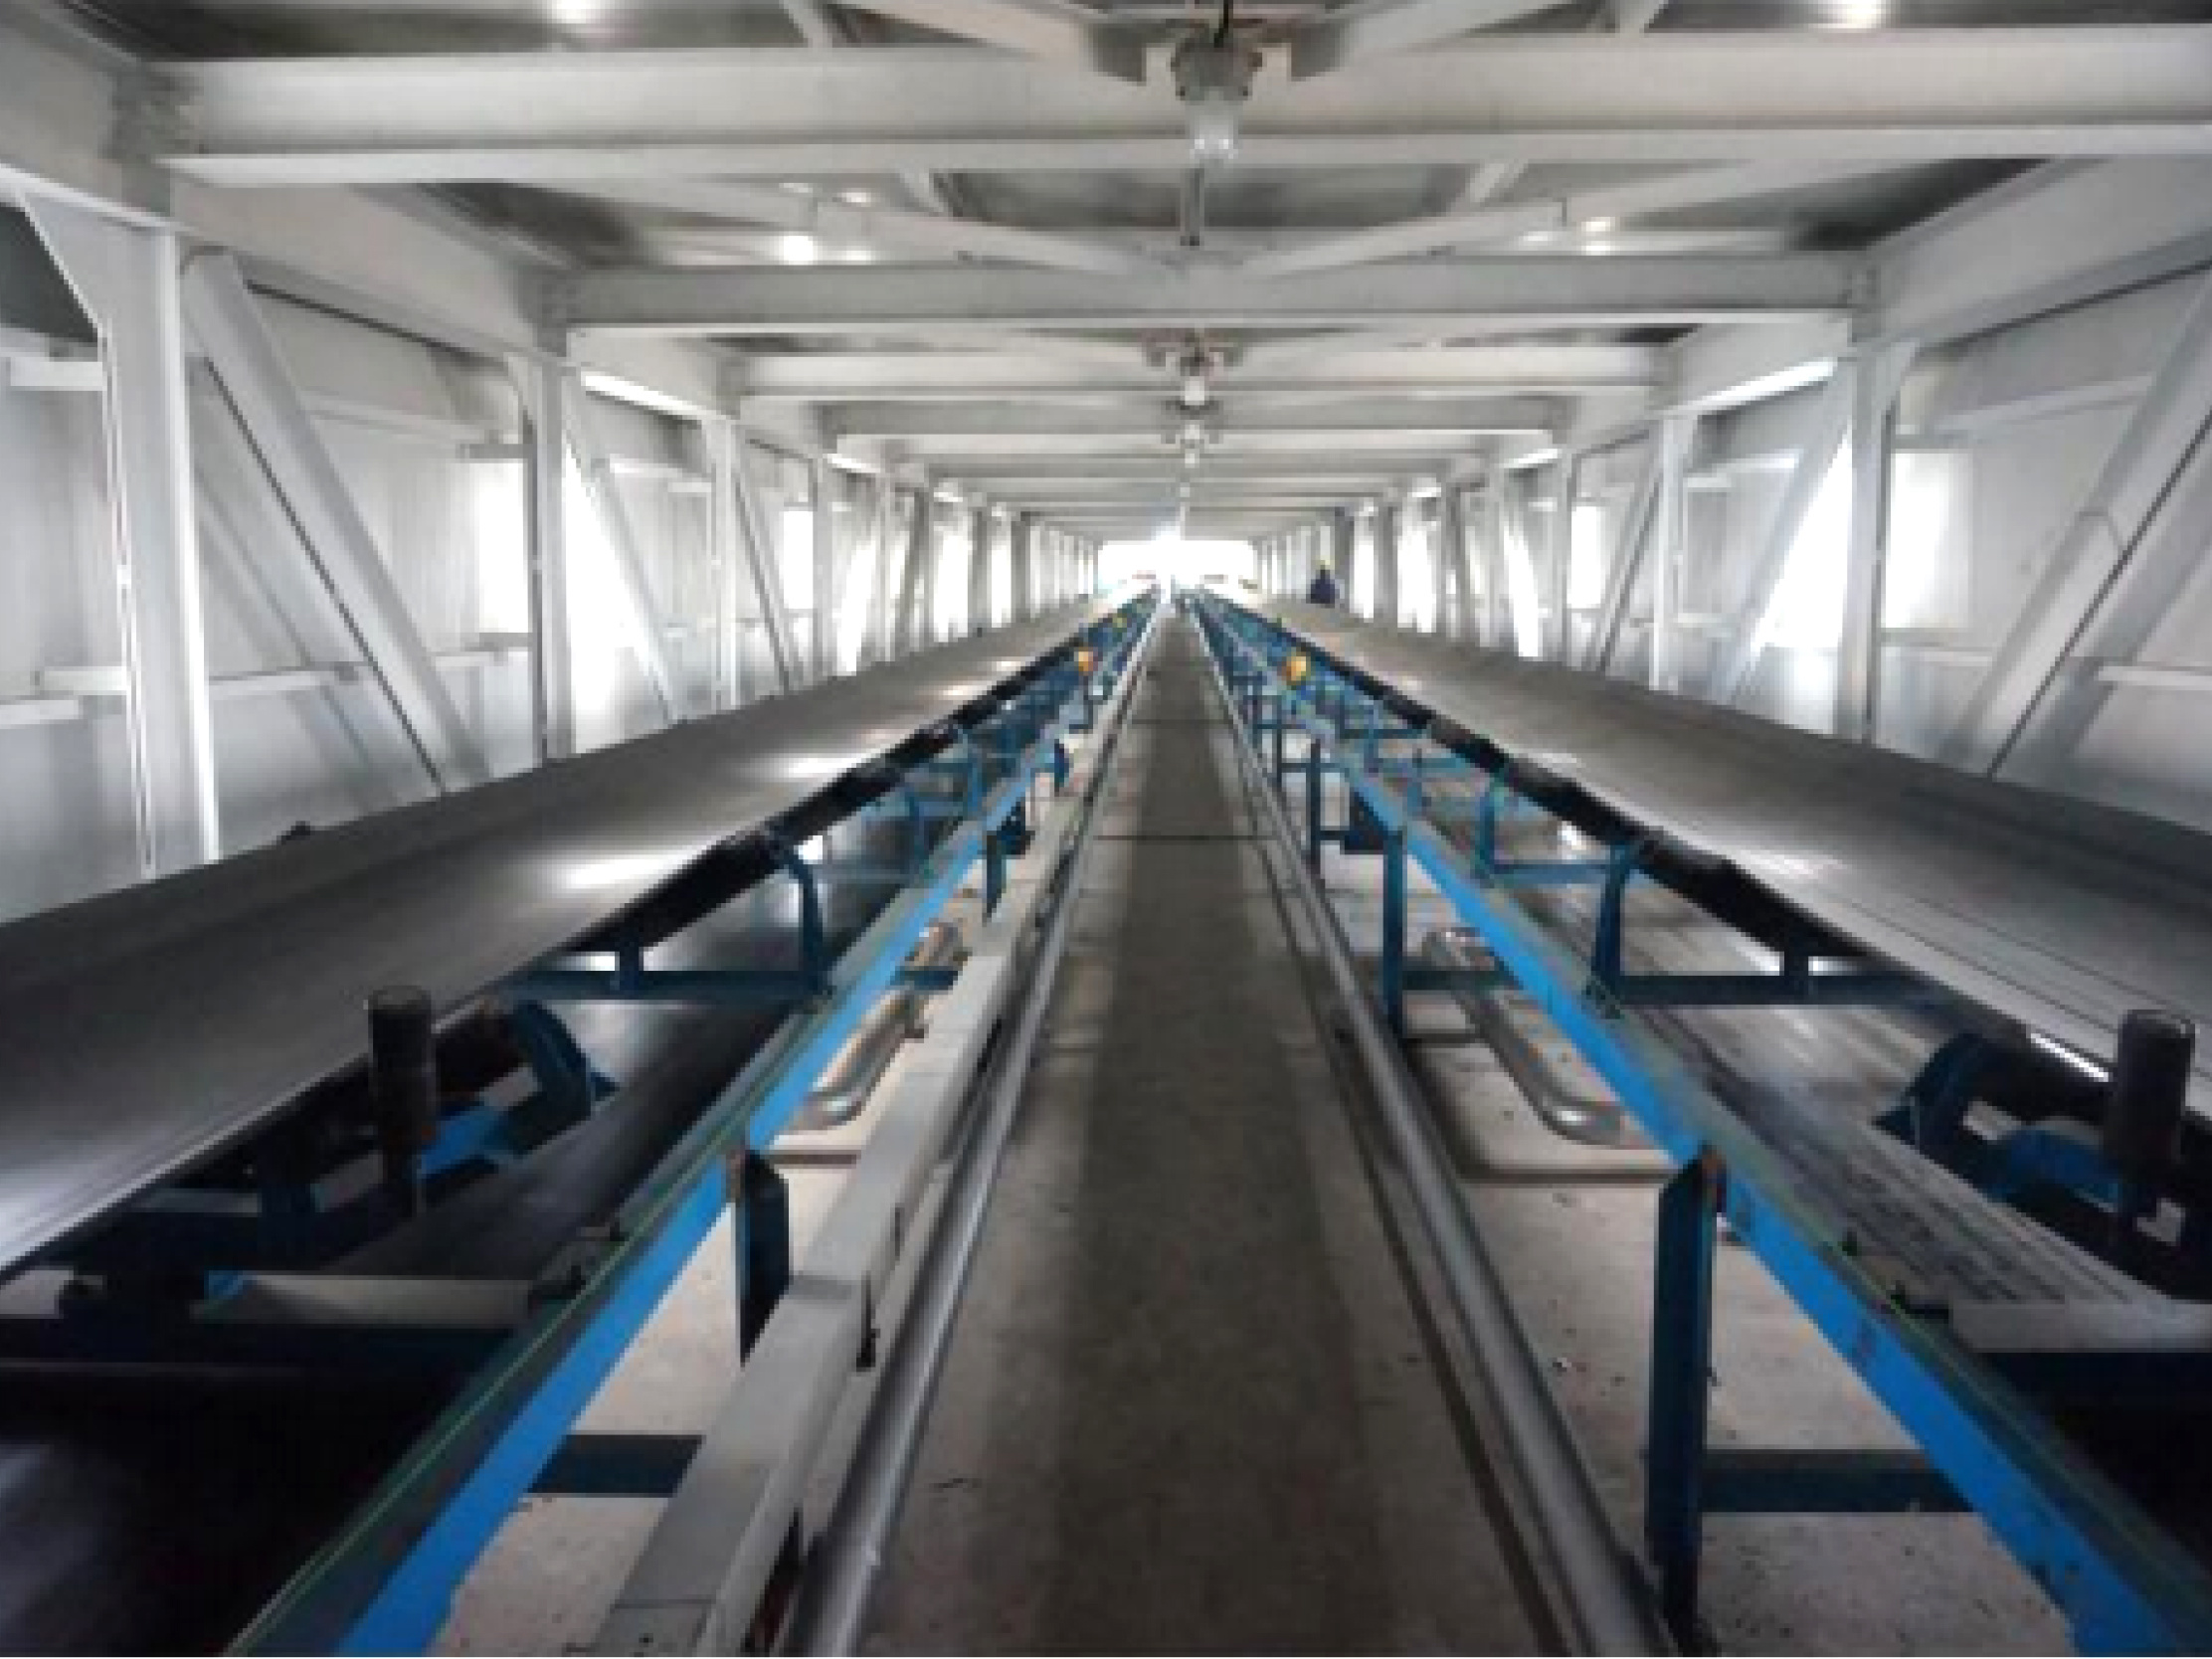
Shaftless screw conveyor equipment represents a significant advancement in the field of material handling solutions, particularly beneficial for transporting bulk materials in an efficient and effective manner. Unlike traditional screw conveyors, shaftless designs eliminate the need for a central shaft, allowing for a more flexible and streamlined operation. This unique design is ideal for handling a wide variety of materials, including those that are sticky, viscous, or prone to clumping, which can often cause challenges in conventional systems.
One of the primary advantages of shaftless screw conveyors is their ability to minimize space requirements while maximizing throughput. The absence of a shaft allows for a smaller diameter design, which can be beneficial in applications where space is limited. Additionally, the shaftless design reduces the risk of material buildup around the shaft, which can often lead to increased maintenance requirements and downtime in traditional systems. This reduction in maintenance not only enhances operational efficiency but also extends the lifespan of the equipment.
Shaftless screw conveyors are particularly effective in industries dealing with difficult-to-handle materials, such as food processing, wastewater treatment, and various recycling applications. Their robust construction allows them to handle high capacities and can be customized to fit specific operational needs. The design facilitates smooth material flow, which is crucial for maintaining process consistency. Furthermore, shaftless screw conveyor equipment can be designed to move materials at various angles, providing flexibility in layout and installation.
Another noteworthy feature of shaftless screw conveyors is their ability to convey materials with high moisture content without the risk of clogging. This is particularly advantageous in applications where moisture retention is a challenge, such as in the conveyance of organic waste or sludge in wastewater facilities. The efficient handling of these materials helps optimize the overall workflow, contributing to improved productivity and reduced operational costs.
Moreover, the easy installation and adaptability of shaftless screw conveyor equipment make it a preferred choice for many industrial applications. The equipment can be seamlessly integrated into existing systems, allowing for upgrades without significant changes to the infrastructure. This adaptability ensures that businesses can improve their material handling processes without incurring substantial capital expenditures.
In summary, shaftless screw conveyor equipment offers a modern solution to the challenges faced in material handling. With advantages such as reduced maintenance, flexibility in design, and enhanced efficiency, it provides an innovative approach for various industries. By understanding the capabilities and benefits of this technology, businesses can make informed decisions that lead to enhanced operational performance and material handling efficiency.
One of the primary advantages of shaftless screw conveyors is their ability to minimize space requirements while maximizing throughput. The absence of a shaft allows for a smaller diameter design, which can be beneficial in applications where space is limited. Additionally, the shaftless design reduces the risk of material buildup around the shaft, which can often lead to increased maintenance requirements and downtime in traditional systems. This reduction in maintenance not only enhances operational efficiency but also extends the lifespan of the equipment.
Shaftless screw conveyors are particularly effective in industries dealing with difficult-to-handle materials, such as food processing, wastewater treatment, and various recycling applications. Their robust construction allows them to handle high capacities and can be customized to fit specific operational needs. The design facilitates smooth material flow, which is crucial for maintaining process consistency. Furthermore, shaftless screw conveyor equipment can be designed to move materials at various angles, providing flexibility in layout and installation.
Another noteworthy feature of shaftless screw conveyors is their ability to convey materials with high moisture content without the risk of clogging. This is particularly advantageous in applications where moisture retention is a challenge, such as in the conveyance of organic waste or sludge in wastewater facilities. The efficient handling of these materials helps optimize the overall workflow, contributing to improved productivity and reduced operational costs.
Moreover, the easy installation and adaptability of shaftless screw conveyor equipment make it a preferred choice for many industrial applications. The equipment can be seamlessly integrated into existing systems, allowing for upgrades without significant changes to the infrastructure. This adaptability ensures that businesses can improve their material handling processes without incurring substantial capital expenditures.
In summary, shaftless screw conveyor equipment offers a modern solution to the challenges faced in material handling. With advantages such as reduced maintenance, flexibility in design, and enhanced efficiency, it provides an innovative approach for various industries. By understanding the capabilities and benefits of this technology, businesses can make informed decisions that lead to enhanced operational performance and material handling efficiency.
Hot Tags:

Contact Us
E-mail:byunfei2000@gmail.com
Wechat/WhatsApp:+86 17324886663
WhatsApp:+86 18738568071
Address:No. 12 Industrial Road, Zhaipo Town, Xinxiang, Henan Province


REQUEST QUOTE
We will contact you within one working day. Please pay attention to your email.